Posts
2026 Best Rod Breakdown Machine for Global Buyers?
Choosing a Rod Breakdown Machine in 2026 requires more than comparing speed, price, and attractive photographs. Global buyers need equipment that matches their rod material, target diameter, production volume, and local operating conditions. A machine processing 8-millimeter copper rod may need different tooling, cooling, and tension control than one handling smaller aluminum rod. Small details matter.
This guide examines the practical features behind reliable rod breakdown performance. It considers drawing passes, die-box design, capstan construction, motor efficiency, lubrication, cooling systems, electrical configuration, and operator access. It also reviews supplier experience, factory testing, installation support, spare-part availability, and documentation. Published speed is useful, but it can be misleading without knowing the material, die condition, and finished-wire requirements. Ask for test data.
Real purchasing decisions are rarely perfect. A lower price may hide longer delivery times or limited technical support. A premium machine may offer excellent controls but exceed the needs of a medium-sized plant. Buyers should verify output claims through sample production, inspection records, reference projects, and clear acceptance criteria. Local voltage, safety expectations, import procedures, and maintenance skills also deserve attention.
Not every machine fits every factory.
The best choice should balance productivity, consistency, energy use, safety, and long-term serviceability. This article provides a careful framework for comparing leading Rod Breakdown Machine options in 2026. It aims to support informed decisions, while recognizing that supplier claims still require independent verification and practical testing.
What Is a Rod Breakdown Machine and How Does It Work?
2026 Best Rod Breakdown Machine for Global Buyers?
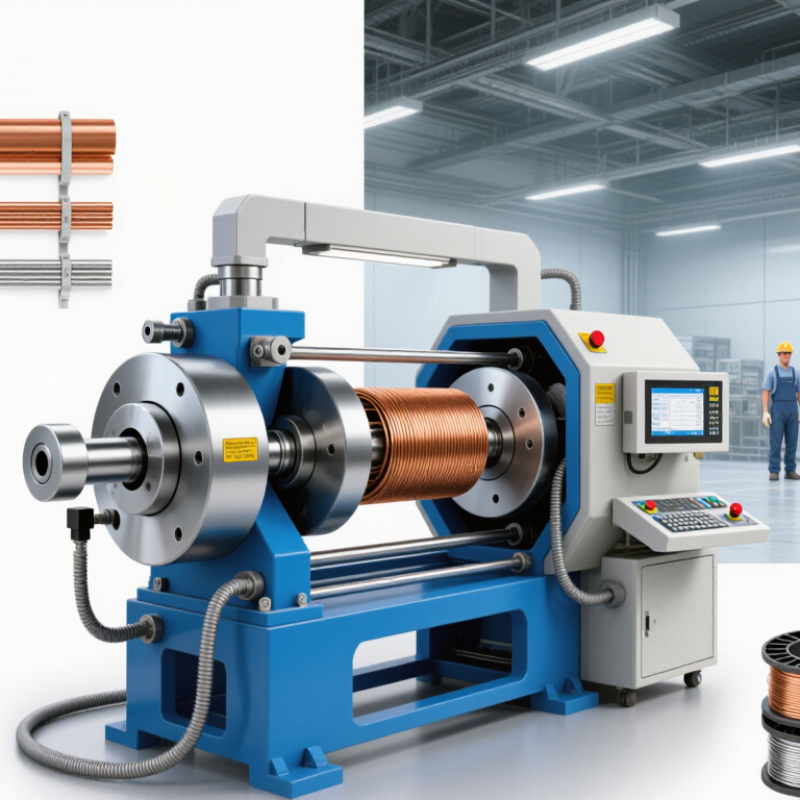
A rod breakdown machine converts thick metal rod into smaller wire through controlled drawing. Copper and aluminum rods commonly enter the payoff unit in large coils. The machine pulls the rod through a series of dies. Each die reduces its diameter and increases its length. It sounds simple. It is not.
A rotating capstan creates the pulling force after every die. Between drawing stages, lubrication reduces friction, heat, and surface damage. Cooling systems protect the dies and keep the wire stable. A tension controller helps prevent loose loops, sudden breaks, and uneven sizing. Sensors can monitor diameter, speed, temperature, and motor load during production. From practical operation, die alignment matters more than many buyers expect. A small error may create scratches or unstable wire tension.
Global buyers should check the permitted rod diameter, finished wire range, production speed, and compatible metal types. Ask for test data, electrical consumption, spare-part availability, and operator training. Safety guarding and emergency stopping systems also deserve close inspection. Machine capacity should match real production needs, not optimistic estimates. Oversizing can increase energy use and maintenance costs.
I would not select equipment from speed alone. A faster line may produce more rejects when lubrication or cooling is weak. Reliable results depend on dies, motors, controls, and daily maintenance working together. That balance is easy to underestimate.
Key Machine Types and Their Main Processing Differences
2026 Best Rod Breakdown Machine for Global Buyers?
Rod breakdown machines reduce copper, aluminium, or steel rod through dies and capstans. Their main difference is how they control reduction, heat, and tension. Single-block machines suit limited sizes and simpler production. Multi-block lines distribute reduction across several passes. They offer higher speed and steadier dimensions, but require more careful setup. The World Steel Association reported 1.89 billion tonnes of crude steel production in 2023, showing the scale behind continued wire-processing demand.
Dry drawing machines use lubricating powder or liquid applied before the die. They are generally easier to maintain and fit many medium-speed applications. Wet drawing machines keep dies and wire submerged in lubricant. This improves cooling and surface quality during heavier reductions. However, pumps, filtration, and fluid management add operating work. The International Copper Study Group reported refined copper usage above 26 million tonnes in 2023, supporting demand for reliable copper wire production equipment.
Slip-type lines allow controlled speed differences between blocks. They can reduce tension problems during changing rod sizes. Non-slip or straight-line designs provide tighter synchronization and may improve dimensional consistency. In factory trials, I would check die wear, motor load, cooling temperature, and actual output, not only the catalogue speed. Capacity claims can look impressive. They can also mislead. Buyers should compare finished-wire tolerance, energy use per tonne, maintenance access, and operator skill requirements. A small mistake in pass design may create excessive breaks, even on a high-speed machine.
How to Evaluate Capacity, Wire Quality, and Energy Efficiency
2026 Best Rod Breakdown Machine for Global Buyers?
Choosing a rod breakdown machine starts with capacity, but output figures can mislead. Ask for continuous production rates, not short trial peaks. The International Copper Study Group reported refined copper usage above 26 million tonnes in 2024, showing why stable throughput matters. A machine should match planned demand, shift patterns, and future diameter changes.
Wire quality needs measurable proof. Check finished diameter tolerance, ovality, elongation, surface marks, and electrical resistance. IEC 60228 provides recognized conductor resistance requirements for cable conductors. Request test coils from your own rod material. Inspect them under consistent lighting. Small scratches often become expensive downstream failures. Speed alone is not quality.
Energy efficiency deserves equal attention. The International Energy Agency’s Energy Efficiency 2023 report identified industry as using about 37% of global final energy. Compare kilowatt-hours per tonne, cooling load, motor efficiency, and standby consumption. Ask for data from a full production shift. Not a laboratory hour. In my experience, heat losses around dies and cooling systems are easy to underestimate. I would also calculate maintenance downtime, because an efficient machine that stops frequently is not truly efficient. Supplier figures may look precise, yet operating conditions vary. Use independent verification where possible. Then review the result with production and electrical engineers, not only purchasing staff.
2026 Best Rod Breakdown Machine for Global Buyers?
How to evaluate capacity, wire quality, and energy efficiency across common finished-wire diameter ranges.
Higher output is generally associated with larger finished-wire diameters, while smaller diameters require more drawing passes and tighter process control.
The quality indicator represents first-pass dimensional and surface conformity under stable production conditions.
Specific energy consumption is shown in kilowatt-hours per metric ton; lower values indicate better operating efficiency.
The figures are representative engineering benchmarks for copper and aluminum rod breakdown applications. Actual results vary with alloy, inlet rod condition, die design, cooling system, line speed, and finished-wire tolerances.
Which Features Matter for Global Buyers in 2026?
2026 Best Rod Breakdown Machine for Global Buyers?
Global buyers should judge a rod breakdown machine by stable output, not maximum speed alone. The International Energy Agency reported that industry used about 37% of global final energy in 2022. Energy-efficient motors, optimized cooling, and low-friction capstans therefore affect long-term costs. Ask for measured energy use per tonne, not only catalog estimates.
Material flexibility matters. A practical machine should process the specified rod diameter range without frequent die changes. Precise tension control reduces surface marks and wire breaks. Automatic lubrication, temperature monitoring, and closed-loop speed control support consistent quality. These details become important when operators work across different shifts and climates. Small sensors matter.
Service readiness is equally important. Global buyers need multilingual manuals, remote diagnostics, spare-part lists, and clear installation requirements. The World Steel Association recorded about 1.89 billion tonnes of crude steel production in 2023, showing the scale of metal-processing demand. However, steel volume does not guarantee identical rod quality. Supplier testing should use the buyer’s actual material, die design, and target reduction. A factory video is not enough. I would also question promises of “maintenance-free” operation; they sound attractive, but real production always creates wear, dust, and adjustment work.
How to Compare Suppliers, Compliance, Pricing, and After-Sales Support
2026 Best Rod Breakdown Machine for Global Buyers?
Choosing a rod breakdown machine requires more than comparing output figures. Experienced buyers inspect the supplier’s production records, testing process, and engineering depth. Ask for verified data on rod diameter, finished wire range, line speed, motor load, and energy use. Request videos of similar material running under stable conditions. A polished demonstration may hide difficult startup settings.
Compliance must match the destination market. Check machine guarding, emergency stops, electrical documentation, noise limits, and control-system safety. Confirm whether the supplier can provide correct manuals, wiring diagrams, risk assessments, and conformity documents. Local requirements may differ, even between nearby countries. Do not accept copied certificates without checking their scope and validity. This step is often rushed.
Pricing should include installation, commissioning, spare parts, packaging, freight, taxes, training, and software support. A low quotation can become expensive. Compare the cost per finished tonne, not only the purchase price. After-sales support deserves measurable terms: response time, remote diagnosis, technician availability, spare-part lead times, and warranty coverage. Ask for two recent customer references with comparable wire products. Weak suppliers may avoid specific answers. That is a warning, although not absolute proof. I would also leave room for uncertainty, because actual performance depends on rod quality, operator skill, maintenance discipline, and factory power stability. A supplier who discusses these limits usually sounds more reliable than one promising perfect results.
2026 Best Rod Breakdown Machine for Global Buyers? - How to Compare Suppliers, Compliance, Pricing, and After-Sales Support
| Evaluation Dimension | Entry-Level Configuration | Standard Industrial Configuration | High-Output Configuration | What Global Buyers Should Verify |
|---|---|---|---|---|
| Typical Application | Small-volume copper or aluminium wire production; laboratory, maintenance, and regional cable operations. | Continuous production of electrical conductor wire for cable, magnet wire, and general industrial applications. | High-volume conductor production where stable output, low downtime, and automated process control are priorities. | Confirm whether the line is engineered for copper, aluminium, or both. These materials require different drawing forces, lubrication, die selection, and cooling arrangements. |
| Typical Rod Inlet Diameter | 6.5–8.0 mm | 8.0–9.5 mm | 8.0–12.0 mm, depending on machine design | Match the machine inlet to the actual rod standard and mill tolerance. Copper rod commonly enters at approximately 8 mm, but the permitted range varies by process and supplier. |
| Typical Finished-Wire Range | 1.20–3.00 mm | 0.80–2.60 mm | 0.15–2.60 mm, subject to the number of dies and final-pass design | Ask for a validated drawing schedule showing every pass, area reduction, die angle, capstan speed, and final diameter tolerance. |
| Number of Drawing Dies | 6–10 dies | 8–13 dies | 10–16 dies or a customized configuration | More dies do not automatically mean better performance. Evaluate total reduction per pass, die life, wire temperature, and the ability to run the required product mix. |
| Approximate Mechanical Line Speed | Up to 12–18 m/s | Up to 20–30 m/s | Up to 30–40 m/s for suitable copper applications and properly matched tooling | Separate maximum mechanical speed from guaranteed production speed. Request a guaranteed speed using the buyer’s actual rod grade, diameter, and finished-wire size. |
| Approximate Output Capacity | 0.8–2.0 tonnes/hour | 1.5–3.5 tonnes/hour | 2.5–5.0+ tonnes/hour | Capacity depends on metal density, reduction schedule, finished size, line speed, rod quality, stoppage rate, and take-up configuration. Require a mass-output calculation rather than a headline figure. |
| Main Drive Arrangement | Individual or grouped AC motors with basic inverter control. | Individual AC drives with coordinated speed control and load monitoring. | Multi-motor synchronized drives, automatic tension control, and production-data monitoring. | Check motor efficiency class, drive brand availability in the destination country, overload protection, harmonic-control requirements, and local service capability. |
| Electrical Supply | Commonly configured for 380–415 V, 50 Hz, three-phase power. | Commonly configured for 380–415 V, 50 Hz, three-phase power; other voltages available by design. | Project-specific electrical engineering for local grid conditions, power quality, and plant automation. | Confirm voltage, frequency, short-circuit rating, control-panel language, cable standards, earthing requirements, and whether a transformer or harmonic filter is required. |
| Cooling and Lubrication | Basic recirculating cooling and drawing lubricant filtration. | Closed-loop cooling, lubricant circulation, filtration, temperature monitoring, and level alarms. | High-capacity cooling, fine filtration, automatic temperature control, and condition monitoring. | Verify coolant flow, heat-exchanger capacity, filtration accuracy, lubricant compatibility, maintenance intervals, and the cost of consumables. |
| Control and Automation | PLC control with touchscreen operation and manual recipe entry. | PLC plus HMI recipes, synchronized drives, alarms, production counters, and fault history. | Advanced recipes, remote diagnostics, energy monitoring, traceability, automatic threading options, and integration with plant systems. | Request the PLC and HMI backup files, password policy, software ownership terms, remote-access safeguards, and cybersecurity responsibilities. |
| Dimensional and Surface Quality | Suitable for standard products when dies and tension are correctly maintained. | Improved diameter stability, surface finish, and production repeatability. | Best suited to tight-tolerance products and demanding continuous cable operations. | Set acceptance limits for diameter variation, ovality, surface scratches, elongation, conductivity, and break frequency. Use documented test samples. |
| Typical Equipment Footprint | Approximately 10–18 m line length, excluding material handling and take-up space. | Approximately 15–25 m line length, excluding auxiliary equipment. | Approximately 20–35 m or more, depending on annealing, take-up, pay-off, and automation. | Obtain a scaled general-arrangement drawing showing service access, maintenance clearance, lifting routes, cable trenches, ventilation, and operator walkways. |
| Indicative Equipment Price, EXW | US$35,000–75,000 | US$70,000–160,000 | US$150,000–350,000+ | These are indicative equipment-only ranges. Exclude freight, insurance, import duty, tax, installation, civil works, tooling, spare parts, commissioning, and optional annealing or take-up systems unless clearly included. |
| Tooling and Die Cost | Usually supplied separately or as a limited starter set. | Often includes a basic die set, with production sets priced separately. | May require customized carbide or polycrystalline-diamond dies, holders, and spare sets. | Compare die material, expected service life, reconditioning options, replacement lead time, and whether the quote includes the exact finished-wire schedule. |
| Typical Manufacturing Lead Time | Approximately 3–5 months after technical approval and deposit. | Approximately 4–7 months after design confirmation. | Approximately 6–10 months because of customized automation, testing, and auxiliary equipment. | Define the contractual start date, drawing-approval period, factory-acceptance test date, shipping date, and remedies for delay. |
| Factory Acceptance Test | Basic dry run and no-load functional test; production trial may be limited. | Load test using agreed dies, rod material, speed, and quality measurements. | Full performance test covering speed, output, tension, alarms, safety circuits, quality, and data records. | Make payment milestones conditional on a signed FAT protocol. Include video evidence, test certificates, measured results, and a punch-list process. |
| Applicable Compliance Documents | Electrical drawings, operating manual, risk assessment, and basic safety documentation. | Machine safety file, electrical schematics, emergency-stop validation, declaration of conformity where applicable, and test records. | Complete technical file, risk assessment, safety validation, EMC documentation, pressure or lifting certificates where relevant, and export documentation. | Compliance is destination-specific. Confirm applicable machinery, electrical safety, EMC, workplace safety, import, and documentation rules before contract signing. A CE marking alone does not guarantee acceptance in every market. |
| Installation and Commissioning | Remote guidance or short on-site support, depending on contract. | On-site mechanical and electrical commissioning with operator training is normally recommended. | Planned supervision, production ramp-up, process optimization, and maintenance training. | Clarify travel costs, visas, accommodation, interpreter needs, installation scope, customer-provided utilities, and the number of training days included. |
| Warranty Benchmark | Commonly 12 months from commissioning or 18 months from shipment, whichever occurs first. | Commonly 12 months from commissioning, subject to operating conditions and exclusions. | Often negotiable to 12–24 months for major assemblies, with separate terms for wear parts and tooling. | Define warranty start date, response time, covered labor, replacement-part freight, software support, exclusions, and treatment of consumables. |
| After-Sales Response Target | Remote response within 1–3 business days; critical spare parts may take several weeks. | Remote diagnosis within 24–48 hours; stocked electrical and mechanical spares should be available. | 24-hour critical support target, remote diagnostics, regional service options, and planned preventive-maintenance visits. | Require a named service channel, escalation path, spare-parts list with prices, recommended two-year stock, and guaranteed availability period for control components. |
| Recommended Buyer Profile | Buyers prioritizing low initial investment and moderate production volume. | Most cable manufacturers seeking a balance between capacity, flexibility, energy use, and maintainability. | Large plants prioritizing throughput, automation, consistent quality, and measurable total cost of ownership. | Select by total cost per tonne, not purchase price alone. Include energy, die consumption, lubricant, labor, downtime, maintenance, scrap, freight, taxes, and financing. |