Posts

How to Choose Vision Inspection Equipment in 2026?

Choosing Vision Inspection Equipment in 2026 requires more than comparing camera resolution or software features. The right system must fit the product, production speed, lighting conditions, and inspection risk. A glossy brochure cannot reveal every weakness.

David Dechow, a respected machine-vision educator, captures this practical reality: “A vision system is only as good as the application it is designed to solve.” That principle should guide every purchase decision. A system inspecting scratched metal parts needs different optics than one checking printed labels. Surface texture, contrast, vibration, and product position can change results within minutes.

Start with the defect. Define its size, location, acceptable variation, and inspection frequency. Then examine the complete setup, including lenses, lighting, cameras, processors, software, conveyors, and rejection devices. A high-resolution camera may still fail under unstable illumination. Small details matter. A loose bracket can create false rejects. Dust can alter readings. Reflections can hide a critical mark.

Reliable Vision Inspection Equipment should also support traceability, recipe changes, data storage, and clear operator feedback. Check compatibility with existing PLCs and manufacturing systems. Review response times, maintenance needs, training requirements, and total ownership costs. The cheapest unit may become expensive after repeated downtime.

Laboratory results are not production results. Factory trials reveal more. Test real samples, including damaged, clean, wet, reflective, and borderline products. Some assumptions will be wrong. That is useful. A careful selection process leaves room for adjustment, honest testing, and measurable improvement.
How to Choose Vision Inspection Equipment in 2026?

What Vision Inspection Equipment Does and Why It Matters

How to Choose Vision Inspection Equipment in 2026?

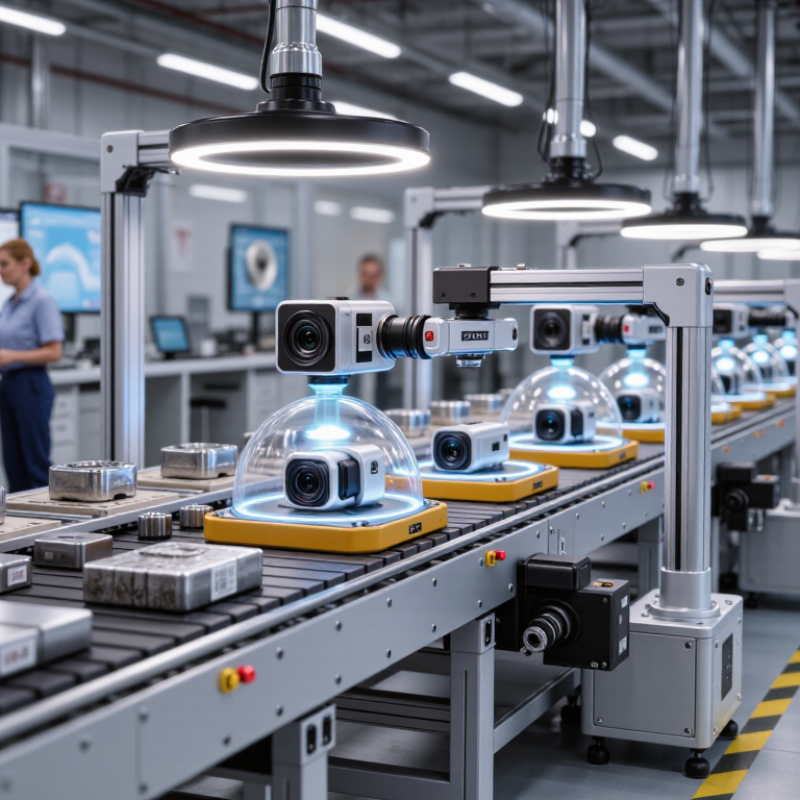
Vision inspection equipment combines cameras, lenses, lighting, sensors, and software. It captures images during production. The system then checks dimensions, surfaces, labels, colors, and assembly details. It can trigger an alarm or remove a failed product within milliseconds. This matters when defects are too small, repetitive, or costly for human inspection. The International Federation of Robotics reported 541,302 industrial robots were installed worldwide in 2023. More automated lines create greater demand for dependable inspection data.

Choose equipment around the defect, not the camera’s advertised resolution. A reflective metal surface may need controlled lighting. A moving part may require a short exposure time. The software must also separate real defects from harmless variation. Grand View Research projects the global machine vision market to grow at an 8.5% compound annual rate from 2024 to 2030. That growth reflects wider adoption, but it does not guarantee good results. A larger market cannot replace careful testing.

Start with production samples, including damaged and borderline parts. Measure false rejects, missed defects, cycle time, and maintenance effort. Keep image records for traceability. Edge processing can reduce network delays, while centralized dashboards support quality analysis. Yet artificial intelligence can still learn the wrong visual pattern. A clean demonstration may mislead. Operators need clear setup instructions and regular validation. The best system is not always the most advanced one. It is the one that remains accurate beside dust, vibration, glare, and changing materials.

How to Define Inspection Goals and Product Requirements

Inspection planning should begin with a measurable defect definition, not a camera specification. Write down the defects, acceptable limits, and inspection frequency. For example, a scratched surface may be unacceptable above 0.5 millimeters. A missing seal may require a zero-tolerance rule. Also record product color, texture, speed, and orientation. These details determine lighting, resolution, triggering, and data storage requirements.

Use production evidence whenever possible. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023 in its World Robotics 2024 report. This growth increases pressure for stable, automated quality checks. However, automation does not repair a vague inspection goal. Define key performance indicators, such as detection rate, false-reject rate, cycle time, and uptime. A target of 99.5% detection may sound strong, but it means little without a defined defect sample and test method.

Build a representative sample set before selecting equipment. Include clean products, borderline defects, reflective surfaces, dust, wrinkles, and normal variation. Test samples from different shifts and suppliers. In practical projects, teams often underestimate product movement and lighting changes. That mistake can make a laboratory trial look excellent. It may fail beside a vibrating conveyor. The 2024 Global Machine Vision Market analysis by Grand View Research identifies quality inspection as a major application area, yet market growth does not guarantee suitability. Leave room for review. Some requirements will change after real production trials.

How to Compare Cameras, Sensors, Lighting, and Software

Choosing vision inspection equipment in 2026 starts with the defect, not the camera. In real production trials, I photograph the smallest acceptable flaw at normal line speed. A high-resolution camera may still fail when vibration, glare, or dust changes the image. Ask for repeatability data, not attractive sample images. Test several parts, including damaged and borderline pieces. Borderline parts matter most.

Compare cameras by resolution, shutter behavior, frame rate, and working distance. A global shutter often handles moving parts better than a cheaper rolling shutter. Sensors should detect position, presence, color, or depth with stable response. Check sensing distance and response time beside the conveyor. Lighting deserves equal attention. Diffused light reduces reflections on curved surfaces, while angled light can reveal scratches. Use adjustable intensity. Fixed brightness may become a problem after maintenance.

Software should connect image rules, alarms, records, and operator access without hiding the logic. During evaluation, change one setting and observe the result across repeated runs. Reliable systems record rejected images and reasons, supporting audits and technician training. Integrate inspection software with existing controls only after testing failure states. A polished demo can mislead. I have learned that setup time is often underestimated. Leave room for calibration, cleaning, recipe changes, and human review. Ask for false-reject data, missed-defect records, and recovery steps in writing.

How to Evaluate Accuracy, Speed, Integration, and Scalability

How to Choose Vision Inspection Equipment in 2026?

Accuracy should be measured on real production samples, not ideal test images. Include surface changes, position shifts, dust, glare, and acceptable defects. Ask suppliers for repeatability data and false-reject rates under your actual lighting conditions. A camera may detect tiny flaws, yet poor lighting can hide them completely. Test several batches. One successful trial proves very little.

Speed must match the full production cycle, including image capture, processing, decision output, and reject timing. Measure performance while the line is running at its highest realistic load. Integration also deserves practical testing. Confirm communication with your control system, trigger sensors, databases, and traceability software. Simple interfaces reduce commissioning time, but “simple” can become limiting later. Review data formats, support responsibilities, and recovery procedures before purchasing.

Tips: Build a scored test plan covering accuracy, cycle time, uptime, and maintenance effort. Use your operators during trials; their experience often reveals awkward cleaning or inspection access. Check how the system handles new products, additional cameras, and changing tolerances. Scalability is not only adding hardware. It includes training, storage, cybersecurity controls, spare parts, and consistent results across multiple lines. Leave room for growth, but avoid paying for unused capacity. I have seen teams prioritize detection precision and underestimate integration delays. That mistake is expensive. Measure everything early.

How to Select, Test, and Maintain Equipment in 2026

How to Choose Vision Inspection Equipment in 2026?

Selecting vision inspection equipment in 2026 starts with the defect, not the camera. Define its size, shape, color, and location on the product. Then match resolution, lens distance, lighting angle, and conveyor speed to that requirement. A shiny surface may need diffused lighting, while a dark edge may need backlighting. Include operators during trials. They often notice handling problems engineers miss.

Testing should use real production samples, including acceptable products and difficult defects. Test under temperature changes, vibration, dust, and normal speed variations. Record false rejects and missed defects separately. A system that performs well for one hour may struggle during an eight-hour shift. I have seen clean laboratory results hide unstable lighting and inconsistent product positioning. That result was useful, but incomplete. Repeat the test after deliberate setup changes.

Maintenance requires more than wiping the lens. Create a schedule for cleaning windows, checking lights, verifying focus, and reviewing inspection logs. Keep reference samples with known defect conditions. Use them during regular performance checks. Calibration records should show the date, operator, settings, and result. Replace aging cables before they create intermittent failures. Software updates also deserve controlled testing. An update may improve detection, yet alter timing or communication. Leave room for human review when the evidence is uncertain. Perfect automation is an attractive idea, but production rarely behaves perfectly.