What Are the Top 10 Types of Auto Arc Welding Machines?
The global welding industry is moving toward faster, more consistent, and better-connected production. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. Many support arc welding, although the report does not separate welding robots from other applications. That limitation matters. Market reports often combine manual, robotic, and automated equipment under one category.
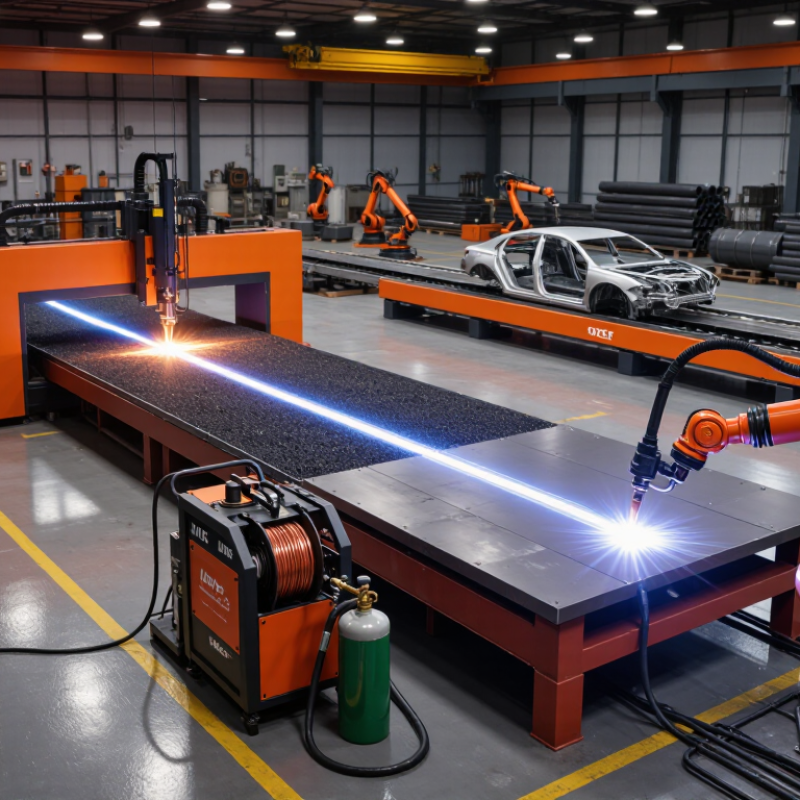
This guide examines the top 10 types of Auto Arc Welding Machine used across fabrication shops, automotive plants, steel structures, and pipeline manufacturing. The list considers welding process, power source, motion system, control method, material compatibility, and maintenance demands. It covers MIG/MAG, TIG, submerged arc, plasma arc, robotic, orbital, and collaborative welding platforms. Each type creates a different shop-floor picture: a torch tracing a programmed seam, a wire feeder clicking beside a fixture, or a robot repeating the same joint for hours.
Practical experience must remain central. AWS welding educator Jerry Uttrachi has emphasized, “Safety is not an option; it is a requirement.” That principle supports the guidance in AWS standards and ISO 14732, which addresses qualification for welding operators using mechanized and automatic equipment. A reliable Auto Arc Welding Machine should deliver stable arc control, repeatable travel speed, accessible controls, and documented inspection procedures. It should also match the joint design, shielding gas, electrode, and operator skill level.
Automation is not automatically better. Sometimes, it adds complexity. The right machine depends on production volume, tolerances, training, and repair access. This overview may simplify a complicated market, but it offers a practical starting point for comparing equipment before purchase.
Classify the Top 10 Machines by ISO 4063 Arc-Welding Process Codes
Auto arc welding machines are best classified by their ISO 4063 process codes, not by appearance or control-panel size. Code 111 identifies manual metal arc machines using coated electrodes, often chosen for repair work and outdoor fabrication. Code 114 covers self-shielded tubular-cored arc welding, useful where wind can disturb external shielding gas. Code 121 represents submerged arc welding with solid wire, delivering deep penetration beneath granular flux. Code 131 describes MIG welding with inert shielding gas and solid wire. Code 135 covers MAG welding with active shielding gas, widely used for carbon-steel production.
The remaining machine types address more specialized conditions. Code 136 is gas-shielded flux-cored arc welding, combining high deposition with strong tolerance for surface variation. Code 137 refers to flux-cored welding with inert shielding gas in applicable process classifications. Code 138 identifies metal-cored arc welding, which can produce smooth, productive welds on suitable steels. Code 141 is TIG welding with a non-consumable tungsten electrode, valued for clean control on thin sections and critical joints. Code 15 covers plasma arc welding, offering a concentrated arc for precision cutting or welding applications. Real workshop selection is less tidy. Wire diameter, joint access, duty cycle, ventilation, and operator skill can change the decision. ISO codes improve technical communication, but they do not replace procedure qualification or hands-on inspection. I would verify the current ISO edition before publishing specifications.
What Are the Top 10 Types of Auto Arc Welding Machines? - Classify the Top 10 Machines by ISO 4063 Arc-Welding Process Codes
Representative ranking based on industrial use, automation suitability, process versatility, and production efficiency
| Rank | ISO 4063 Code | Automated Machine Type | ISO 4063 Process Classification | Electrode or Filler | Shielding Method | Typical Automation Format | Common Applications | Main Production Advantage |
|---|---|---|---|---|---|---|---|---|
| 1 | 135 | Automated MAG Solid-Wire Welding Machine | MAG welding with a solid wire electrode | Continuously fed solid consumable wire | Active shielding gas, commonly argon-based mixtures with carbon dioxide | Robotic arm, welding gantry, or multi-axis production cell | Automotive components, machinery, structural fabrication, and general steel assemblies | High deposition efficiency, precise wire control, and easy integration with robots |
| 2 | 121 | Automatic Submerged Arc Welding Machine | Submerged arc welding with a solid wire electrode | Continuously fed solid wire electrode | Granular fusible flux covering the arc | Column-and-boom system, tractor, or longitudinal welding line | Pressure vessels, large beams, storage tanks, ship sections, and long seams | Very high deposition rate, deep penetration, and low visible arc exposure |
| 3 | 136 | Automated MAG Flux-Cored Welding Machine | MAG welding with a flux-cored wire electrode | Continuously fed tubular flux-cored wire | Externally supplied active shielding gas plus flux ingredients in the wire | Robotic welding cell, seam-tracking gantry, or automated positioner | Heavy equipment, shipbuilding, structural steel, and high-strength steel fabrication | High deposition, good tolerance of surface contamination, and strong weld performance |
| 4 | 131 | Automated MIG Solid-Wire Welding Machine | MIG welding with a solid wire electrode | Continuously fed solid consumable wire | Inert shielding gas, typically argon or helium-based gas | Robotic arm, automated rotary table, or Cartesian welding system | Aluminium parts, stainless steel assemblies, vehicle components, and thin-to-medium sections | Clean arc operation, high travel speeds, and excellent suitability for non-ferrous metals |
| 5 | 141 | Automated TIG Welding Machine | TIG welding with a non-consumable tungsten electrode | Non-consumable tungsten electrode; separate filler wire may be added | Inert shielding gas, normally argon or helium | Orbital welding head, robotic torch, or precision rotary welding system | Stainless steel tubing, aerospace parts, food-processing equipment, and precision pipe joints | Excellent weld appearance, accurate heat control, and low spatter |
| 6 | 138 | Automated MAG Metal-Cored Welding Machine | MAG welding with a metal-cored wire electrode | Continuously fed tubular metal-cored wire | Externally supplied active shielding gas | Robotic cell, tandem-wire system, or automated production line | Automotive frames, heavy machinery, structural fabrication, and repetitive fillet welds | High deposition with good arc stability and reduced slag compared with many flux-cored processes |
| 7 | 151 | Automated Plasma Arc Welding Machine | Plasma arc welding | Non-consumable tungsten electrode; filler wire may be used | Plasma gas and shielding gas, generally inert gases | Precision robotic cell, orbital system, or automated keyhole welding unit | Thin stainless steel, aerospace components, tubing, and precision fabrication | Concentrated high-energy arc, stable penetration, and suitability for precision welds |
| 8 | 122 | Automatic Submerged Strip-Electrode Welding Machine | Submerged arc welding with a strip electrode | Continuously fed metal strip electrode | Granular submerged welding flux | Automated cladding head, longitudinal welding machine, or strip-overlay system | Corrosion-resistant overlays, pressure equipment, chemical vessels, and large surfaces | Wide, uniform weld beads and high productivity in surfacing operations |
| 9 | 114 | Automated Self-Shielded Flux-Cored Arc Welding Machine | Self-shielded tubular-cored arc welding | Continuously fed self-shielded flux-cored wire | Shielding generated by flux ingredients in the wire; no external gas required | Rail-mounted welding tractor, outdoor gantry, or mechanized structural welding system | Outdoor construction, bridges, heavy structural steel, and sites exposed to wind | Good outdoor performance because the process does not depend on an external shielding-gas supply |
| 10 | 111 | Mechanized Manual Metal Arc Welding Machine | Manual metal arc welding with a covered electrode | Flux-covered, consumable stick electrode | Shielding generated by the decomposition of electrode coating | Mechanized electrode holder, welding tractor, or purpose-built repetitive weld fixture | Repair welding, heavy maintenance, field fabrication, and difficult-access joints | Simple equipment, strong outdoor capability, and compatibility with many steel grades |
Note: ISO 4063 process codes identify the welding process rather than a specific machine design. Actual equipment may combine a power source, wire or electrode feeder, torch, motion system, positioner, sensors, and process-control software.