Posts

What Is Plastic Parts Manufacturing and How Does It Work?

Plastic parts manufacturing turns polymer materials into components designed to fit, move, seal, or protect. It supports products as varied as appliance housings, automotive clips, packaging, and medical-device components. The work involves more than shaping melted resin. Engineers must match the material and part design to production needs and the conditions the finished component will face.

A typical project begins with clear requirements: dimensions, expected loads, temperature exposure, appearance, and target cost. Designers then select a polymer and forming process. Injection molding is common for detailed parts made in repeated runs. Extrusion produces continuous profiles, while thermoforming shapes heated plastic sheets over a mold. Each method has limits. Thin walls may cool unevenly, sharp corners can concentrate stress, and complex tooling can add significant upfront cost. Small choices matter.

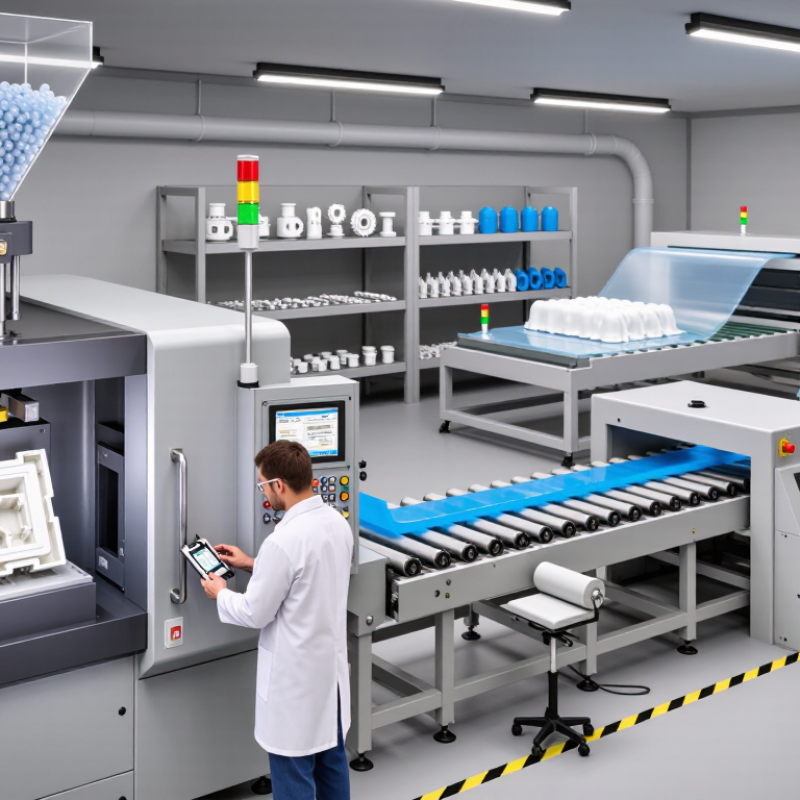
Production generally includes preparing material, forming the part, cooling or curing it, removing it from the tool, and checking key features. Quality checks may include dimensional measurements, surface inspections, and fit or strength tests. A part that looks right can still fail after repeated heat or loading. That matters. Reliable results depend on suitable tooling, controlled production conditions, accurate drawings, and communication between designers and manufacturers—not machinery alone.

This guide explains how plastic parts manufacturing works, what common processes involve, and how teams choose materials and methods. No single approach suits every part. Early assumptions should be checked against the component’s real purpose.
What Is Plastic Parts Manufacturing and How Does It Work?

What Plastic Parts Manufacturing Involves

Plastic parts manufacturing turns a design into repeatable components through material selection, tooling, forming, and inspection. Engineers choose a polymer based on strength, flexibility, heat exposure, and expected production volume. They then refine the part geometry and create a mold or other forming tool. Common methods include injection molding, extrusion, blow molding, and thermoforming. Each suits different shapes and production needs.

During molding, plastic is heated, shaped, and cooled; operators then trim excess material and check dimensions, surface finish, and fit. Small details matter. A thin wall may cool unevenly, while a sharp corner can concentrate stress. Process settings also affect consistency, so teams typically test sample parts before routine production. The scale of the industry makes these choices consequential: the OECD reported that global plastics production reached 460 million tonnes in 2019, while plastic waste reached 353 million tonnes; only 9% was recycled. That context makes material efficiency and avoidable scrap worth considering early, though design trade-offs are rarely simple.

Tip: Confirm wall thickness, draft angles, and critical tolerances with the manufacturer before tooling. A small design change can simplify production, but it may also affect strength or appearance. Fit is unforgiving.

What Is Plastic Parts Manufacturing and How Does It Work?

Injection molding heats plastic pellets until they melt, injects the material into a mold, and cools it to form a part. The chart shows typical melt-temperature ranges for several commonly used thermoplastics.

Temperatures are approximate ranges in °C; the appropriate setting depends on the specific grade, equipment, and processing conditions.

Which Materials Are Used to Make Plastic Parts

Plastic parts usually use thermoplastics because heat can soften them for molding, then they harden as they cool. Common choices include polyethylene and polypropylene for lightweight, moisture-resistant parts; ABS for impact-resistant housings; and polycarbonate for clear, tough components. Nylon and acetal suit moving parts, though moisture and friction can affect their performance. It depends on the job. Thermosets, such as epoxy and phenolic resins, hold their shape under heat but cannot be remelted like thermoplastics.

Material selection also considers temperature, chemicals, load, appearance, and manufacturing method. Glass fibers can stiffen nylon, while mineral fillers may reduce cost or change warpage. Additives can improve color, UV resistance, or flame performance, but they may complicate recycling. PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023, showing the scale of material choices. The OECD’s Global Plastics Outlook reported that only 9% of plastic waste was recycled in 2019. Recycled resin can vary between batches, so parts with tight tolerances need testing. That trade-off is easy to overlook. The best material is not always the strongest; it must perform reliably in the finished part.

What Is Plastic Parts Manufacturing and How Does It Work? - Which Materials Are Used to Make Plastic Parts

Plastic parts manufacturing converts polymer materials into components through processes such as molding, extrusion, and thermoforming. Material and process choices depend on the part’s shape, performance requirements, production volume, and cost.

Material Material type Typical characteristics Common manufacturing processes Typical uses and considerations
Polypropylene (PP) Thermoplastic Low density, good chemical resistance, and good fatigue resistance; can become brittle at low temperatures. Injection molding, extrusion, and blow molding Containers, closures, living hinges, and housings. Often selected for lightweight parts that contact chemicals.
Polyethylene (PE) Thermoplastic; includes HDPE and LDPE grades Good moisture and chemical resistance. Stiffness and flexibility vary by grade. Extrusion, blow molding, and injection molding Bottles, containers, tubing, and film. Grade selection affects stiffness, toughness, and processability.
Acrylonitrile Butadiene Styrene (ABS) Thermoplastic Tough, impact-resistant, and readily molded; heat and outdoor weather resistance depend on grade. Injection molding and extrusion Enclosures, housings, and interior components. Not usually the first choice for prolonged outdoor exposure without a suitable grade or protection.
Polycarbonate (PC) Thermoplastic High impact strength and transparency; can be sensitive to scratching and some chemicals. Injection molding and extrusion Protective covers, transparent components, and lighting parts. Drying before processing is commonly required to reduce moisture-related defects.
Polyamide (PA, Nylon) Thermoplastic Good strength, wear resistance, and performance in moving parts; absorbs moisture, which can affect dimensions and properties. Injection molding and extrusion Gears, clips, bearings, and mechanical components. Moisture conditioning and grade selection may be important for dimensional control.
Polyoxymethylene (POM, Acetal) Thermoplastic Stiff, dimensionally stable, and low-friction, with good wear properties. Injection molding and extrusion Precision gears, rollers, and sliding parts. Its chemical compatibility should be checked for the intended environment.
Polyvinyl Chloride (PVC) Thermoplastic; available in rigid and flexible formulations Good chemical and weather resistance in suitable formulations; properties vary with additives and grade. Extrusion and injection molding Pipes, profiles, fittings, and flexible components. Processing requires control of heat to avoid material degradation.
Polyethylene Terephthalate (PET) Thermoplastic polyester Good strength and barrier properties; moisture control during processing is important. Injection molding, extrusion, and stretch blow molding Bottles, packaging, and fibers. The required grade and process depend on the part’s intended use.
Phenolic resin Thermosetting plastic Retains its shape after curing and can provide heat resistance and electrical insulation; generally less ductile than many thermoplastics. Compression molding and transfer molding Electrical components and heat-resistant parts. Cured thermosets cannot be remelted and reshaped like thermoplastics.

Typical workflow: Define part requirements → select a material and process → design and make tooling → form the part → cool or cure it → trim and inspect it. Actual properties vary by grade, additives, part design, and processing conditions.

How a Plastic Part Is Designed and Prepared

A plastic part’s performance is shaped long before it reaches a molding machine. Designers begin with its purpose, expected loads, operating temperature, and contact with other components. They then build a CAD model with practical wall thicknesses, rounded corners, and draft angles so the part can release from a mold. Small details matter. A sharp internal corner may concentrate stress, while an uneven wall can cool inconsistently and cause sink marks or warping. Material choice also affects flexibility, strength, shrinkage, and surface finish.

The design is reviewed for manufacturability before tooling begins. Engineers check the parting line, gate location, ejector-pin areas, and dimensional tolerances against the component’s function. A snap-fit, for example, needs enough flexibility to assemble without cracking, but its fit should be tested rather than assumed. Prototypes can reveal awkward assembly or weak spots that a screen cannot. They add time, yet skipping them can be more costly. Even a careful review may miss something; production feedback should inform later revisions.

Tips: Keep critical dimensions limited to features that truly need tight control. Mark cosmetic surfaces clearly, and discuss material and finish requirements early. Ask for a design-for-manufacturing review before approving tooling. A simple test fit can catch a surprisingly stubborn problem.

How Plastic Parts Are Formed and Finished

Plastic parts are formed by shaping softened polymer inside or over a tool. In injection molding, heated resin is pushed into a closed metal mold. The material fills narrow channels, then cools until it holds the cavity’s shape. Heat and pressure do the forming. Tool temperature and cooling time affect surface quality and dimensions. A part may shrink slightly as it cools, so mold design often allows for that change. Thin walls can cool unevenly. That can cause warping, even when the part looks sound at first glance. Thermoforming offers another route: a heated plastic sheet is drawn over a mold to create trays, covers, and panels.

Forming is only part of the job. Workers may trim excess material, remove injection points, smooth sharp edges, or drill precise holes. Some parts are joined by welding or fitted with inserts. These steps need care. A rough cut can leave a visible edge, while too much finishing can change a tight fit. Inspection may include checking dimensions with calipers and looking for sink marks, bubbles, or scratches under good light. A drawing can seem complete, yet assembly may reveal a small interference. That is worth checking early. Surface texture and color can also vary between batches, so samples should be reviewed under consistent lighting.

How Manufacturers Inspect and Apply Plastic Parts

Plastic parts inspection begins with the drawing and the part’s intended use. Inspectors check dimensions with calipers, gauges, or optical systems, depending on the required tolerance. Small details matter. A warped edge can prevent a housing from sealing, while a rough gate mark may interfere with assembly. Teams also look for cracks, discoloration, bubbles, and short shots under consistent lighting.

Measurements alone are not enough. Material and process checks can reveal brittleness, uneven wall thickness, or changes between production batches. Sampling plans help manage large runs, but sampling can miss a rare defect; critical features may need more frequent checks. Records should connect results to the batch, inspection method, and acceptance limits. Even a careful checklist can be wrong if its limits do not reflect real use.

Application testing shows whether a part performs after installation. Technicians may fit it into a mating component, apply the expected load, and check for movement, leakage, or stress whitening. Heat, moisture, and repeated assembly can change how plastic behaves. A part that fits on the bench may become loose after cycling. That gap deserves investigation, not a quick adjustment to the drawing. Teams should review failures with production and design staff, then verify any process change on new samples.